Drawing-Based OEM Machining
Manufacture to your 2D drawing, 3D model, material call-out and revision level.

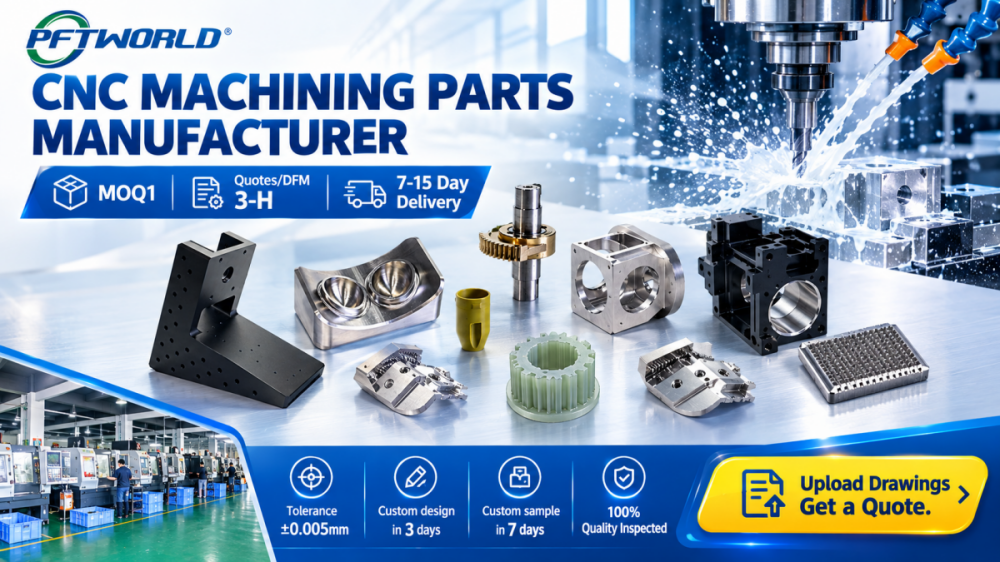
Need a stainless steel block with threaded ports, mounting holes, recessed features or multi-face geometry? Shenzhen Perfect Precision Products manufactures drawing-based CNC milled metal components for OEM equipment, fluid-control assemblies, automation systems and other industrial products. The parts shown here are compact machined blocks with internal threads, through holes, bosses and milled recesses; final dimensions and application requirements are confirmed from your engineering data.
Manufacture to your 2D drawing, 3D model, material call-out and revision level.
CNC milling for prismatic blocks, threaded bores, recessed pockets, bosses and mounting-hole patterns, subject to DFM review.
The factory lists stainless steel grades including 316; confirm the exact 316L grade and material certificate requirement for your project.
ISO9001:2015 and ISO13485:2016 certificates are documented in the supplied company records; QC resources include CMM and 2D measuring instruments.
Low-quantity prototype work and production orders are reviewed according to geometry, quantity, finish and inspection requirements.
Send the drawing, model or dimensioned sample information. The engineering team can review manufacturability, identify missing requirements and return a quotation with clear assumptions before production is confirmed.
| Specification | Product-Page Status |
|---|---|
| Part type | Custom CNC milled stainless steel block / port and mounting component; exact part name subject to drawing review. |
| Material | 316L stainless steel according to the supplied product reference; confirm grade with the drawing and material certificate before publication. |
| Material condition | To be confirmed by project specification. |
| Manufacturing process | CNC milling with drilling, tapping and multi-side machining as required by geometry; exact routing subject to DFM review. |
| Visible features | Internal threaded bores, through holes, recessed or stepped pockets, circular boss, mounting holes and milled outer profiles. |
| Dimensions | To be confirmed from a 2D drawing or 3D CAD model; do not infer dimensions from product references or ruler images. |
| Product-specific tolerances | To be confirmed from the drawing and quotation. |
| General factory tolerance capability | Standard machining tolerance ±0.01 mm; special precision areas ±0.005 mm, depending on material, geometry and size. This is a general factory capability, not a confirmed tolerance for every feature shown. |
| Surface roughness | General factory capability Ra 0.1–3.2 µm depending on feature and finish requirement; product-specific value to be confirmed. |
| Thread standard | To be confirmed: metric, UNC/UNF, BSP, NPT or another standard. Include nominal size, pitch, class and effective depth on the drawing. |
| Surface treatment | Project-dependent. Available factory options include polishing, plating, powder coating, black oxide and other coordinated finishes; confirm suitability for 316L and the required standard before quotation. |
| Deburring | Required and to be defined by drawing or purchase specification, especially around threaded ports, cross holes and sealing surfaces. |
| Inspection | Incoming material inspection, first-article inspection, in-process or sampling inspection and pre-shipment inspection are documented factory procedures. |
| Inspection equipment | CMM and 2D measuring instruments are documented; additional gauges and third-party inspection can be discussed for project requirements. |
| Material documentation | Material certificates or mill test reports can be requested. Specify the required grade and certificate type, such as EN 10204 3.1, at inquiry stage. |
| Order quantity | Flexible and project-dependent; prototype and small-batch CNC quantities can be discussed. |
| Prototype support | Available. Simple CNC prototypes may be delivered in 1–3 days; standard prototypes typically require 1–2 weeks, depending on complexity, material, finish and inspection. |
| Production option | Pilot and repeat production available subject to capacity planning and drawing review; standard production lead time is typically 3–4 weeks for standard orders, project-dependent. |
| Drawing formats | PDF, STEP, IGES/IGS, STL, X_T, DWG and DXF are listed as accepted engineering formats; ideally provide both a 3D model and a 2D drawing. |
| Packaging | To be defined by the part’s surface protection, cleanliness, quantity and shipping requirements. |
Incorrect thread type, pitch or effective depth can stop a component from fitting even when the outside dimensions look correct. Provide the thread standard, nominal size, pitch, depth, entry chamfer and any sealing requirement on the drawing. The engineering review can then confirm tool access and inspection requirements before machining.
The components combine features on different faces, including front ports, upper openings, recessed areas and mounting holes. The factory supports CNC milling across 3-, 4- and 5-axis equipment; the recommended setup depends on the number of datums, required perpendicularity and the production quantity.
The supplied product reference identifies 316L stainless steel, while the company capability records list stainless steel grades including 316. To protect material traceability, specify the exact grade and required documentation in the RFQ. Material certificates and batch traceability can be requested subject to project scope and documentation requirements.
Deep pockets, internal corners, cross-drilled passages, small holes and closely spaced mounting patterns can affect tooling access, cycle time and cost. The factory’s DFM review covers achievable tolerances, internal radii, deep features, thread types and cost-optimization opportunities. Feedback is provided with the quotation for quotation projects.
For a port or mounting block, the critical features are normally defined by the drawing: port location, thread size and depth, hole pattern, boss position, datum relationships and sealing surfaces. The documented four-stage QC process includes incoming material inspection, first-article inspection, in-process or sampling inspection and pre-shipment inspection, with CMM and 2D measuring resources available.
A prototype should be manufactured with the same functional requirements that will govern later production wherever practical. The factory supports prototype, pilot and repeat-production discussions; the confirmed schedule depends on material availability, geometry, quantity, finish and inspection documentation.
If the product includes machined metal parts, molded components or sheet-metal covers, the factory can review multiple process types under an OEM/ODM program. Each part still requires its own drawing, specification and price; assembly-level fit requirements must be included in the assembly drawing.
Review the 2D drawing, 3D model, material grade, critical dimensions, datums, thread call-outs, finish and inspection requirements. The team identifies missing information and potential risks before quotation.
Confirm the material grade and documentation requirement. For 316L projects, specify whether an MTR/MTC, chemical composition, mechanical properties, heat or lot traceability or EN 10204 3.1 documentation is required.
The process may include stock preparation, face milling, pocketing, drilling, tapping, boring and multiple-side machining. The exact process plan is selected from the part geometry and drawing requirements; product references alone do not establish the final routing.
Remove machining burrs and define edge-break requirements on the drawing. Thread entrances, cross holes, recessed pockets and sealing areas require particular attention.
If the project requires polishing, plating or another finish, state the required appearance, coating or finish standard and protected areas. Surface treatments are coordinated according to project requirements; any finish that affects threads or critical dimensions should be identified before quoting.
The factory documents first-article, in-process or sampling and pre-shipment inspection. CMM and 2D measuring instruments can support dimensional verification; the required report type and sampling plan should be agreed before production.
Finished parts are checked against the agreed specification before packing. Packaging should be selected according to thread protection, scratch risk, cleanliness, quantity and destination requirements.
Quality scope: ISO9001:2015 and ISO13485:2016 are documented factory-level quality certifications. They support the manufacturing system but do not automatically certify this specific component for a regulated end use.
The company knowledge base identifies medical, aerospace, automotive, marine, robotics and automation, agricultural machinery, industrial equipment and electronics as target industries for its broader manufacturing services.
This does not mean that the pictured component is approved for every listed industry. The end use and qualification requirements must be reviewed for each project.
These application descriptions are engineering hypotheses based on visible port, hole and mounting geometry. The page should not claim pressure service, medical use, aerospace approval, FDA or CE status or customer approval without a product-specific specification and supporting documentation.
For an accurate quotation, send:
Accepted engineering formats listed in the company materials include PDF, STEP, IGES/IGS, STL, X_T, DWG and DXF. If drawings are not available, photographs, physical samples or dimensioned sketches may support an initial feasibility review, but final pricing and production approval require adequate dimensional and material information.
Shenzhen Perfect Precision Products Co., Ltd. is documented as an OEM/ODM custom manufacturer rather than only a trading company.
The supplied company records document 79+ machines, including 3/4/5-axis CNC, injection molding and sheet-metal capabilities, with 100+ professional staff.
ISO9001:2015 certification covers CNC precision machining of hardware. ISO13485:2016 is documented for quality management activities related to production, processing and sales of CNC precision parts for medical devices.
The company documents 6 QA/QC inspectors, 5 testing instruments, CMM and 2D measuring instruments, plus a four-stage inspection workflow.
DFM review, drawing review, prototype support and quotation based on drawings, models, samples or photographs are documented capabilities.
The factory reports monthly output above 300,000 pieces across its broader operation; capacity allocated to this component must be confirmed by quantity, geometry and schedule.
The company records customers in 100+ countries and regions and a Hong Kong trading arm for export logistics. Destination-specific Incoterms, freight and documentation are confirmed per quotation.
Customer drawings and product information are treated as confidential business information; an NDA can be requested before sharing project files.
The supplied product reference identifies 316L stainless steel, and the factory capability records include 316 stainless steel among machinable grades. The exact grade for the order must still be confirmed on the engineering drawing and supported by the required material certificate or mill test report.
The references show threaded bores, through holes, recessed features, bosses and mounting-hole patterns. CNC milling, drilling and tapping are documented factory processes. The final thread form, size, depth, tolerance and inspection method must be specified on the drawing.
The documented general factory capability is ±0.01 mm standard machining tolerance, with ±0.005 mm available for special precision areas depending on material, geometry and size. These figures are not a blanket promise for every feature; the drawing must be reviewed to confirm achievable tolerances and cost.
Material certificates or mill test reports can be requested for the material used. Inspection reports can also be provided according to the agreed scope. Specify the required grade, certificate type, sampling plan and report format in the RFQ; EN 10204 3.1 can be discussed where applicable.
Yes. Custom CNC machining is project-dependent and prototype or small-batch quantities can be discussed. Simple CNC prototypes may be completed in 1–3 days, while standard prototypes commonly require 1–2 weeks after engineering review, depending on material, complexity, finish and inspection requirements.
Standard production orders typically require 3–4 weeks, subject to quantity, process complexity, material availability, surface treatment, inspection and current workload. A confirmed shipment date is provided after the drawing and production plan are reviewed.
Photographs, physical samples or dimensioned sketches can support an initial feasibility review or budgetary estimate. For final pricing and production, the factory needs enough information to establish dimensions, threads, material, finish, quantity and inspection requirements.
The company materials list PDF, STEP, IGES/IGS, STL, X_T, DWG and DXF among accepted engineering formats. Ideally, send both a 3D model and a 2D drawing with tolerances, material, finish and quantity call-outs.
Yes. DFM review is documented as part of the quotation engineering service. The review may cover internal radii, deep features, thread access, achievable tolerances, datum strategy and cost-optimization opportunities while preserving the functional requirements.
Customer drawings, product information and designs are treated as confidential business information. An NDA can be requested before file sharing, and project information is restricted to the relevant project team according to the company’s stated practice.
Whether you need one prototype, a small pilot batch or repeat production, the next step is a drawing-based review. Share the 2D drawing, 3D model or dimensioned sample information together with the 316L grade, thread requirements, quantity, finish and target date.
Shenzhen Perfect Precision Products will review the manufacturability of the port and mounting features, identify missing specifications and prepare a quotation based on the confirmed scope.
Custom OEM/ODM CNC machining for drawing-based stainless steel components. Final tolerances, materials, finishes, inspection documents and delivery dates are confirmed per project.


